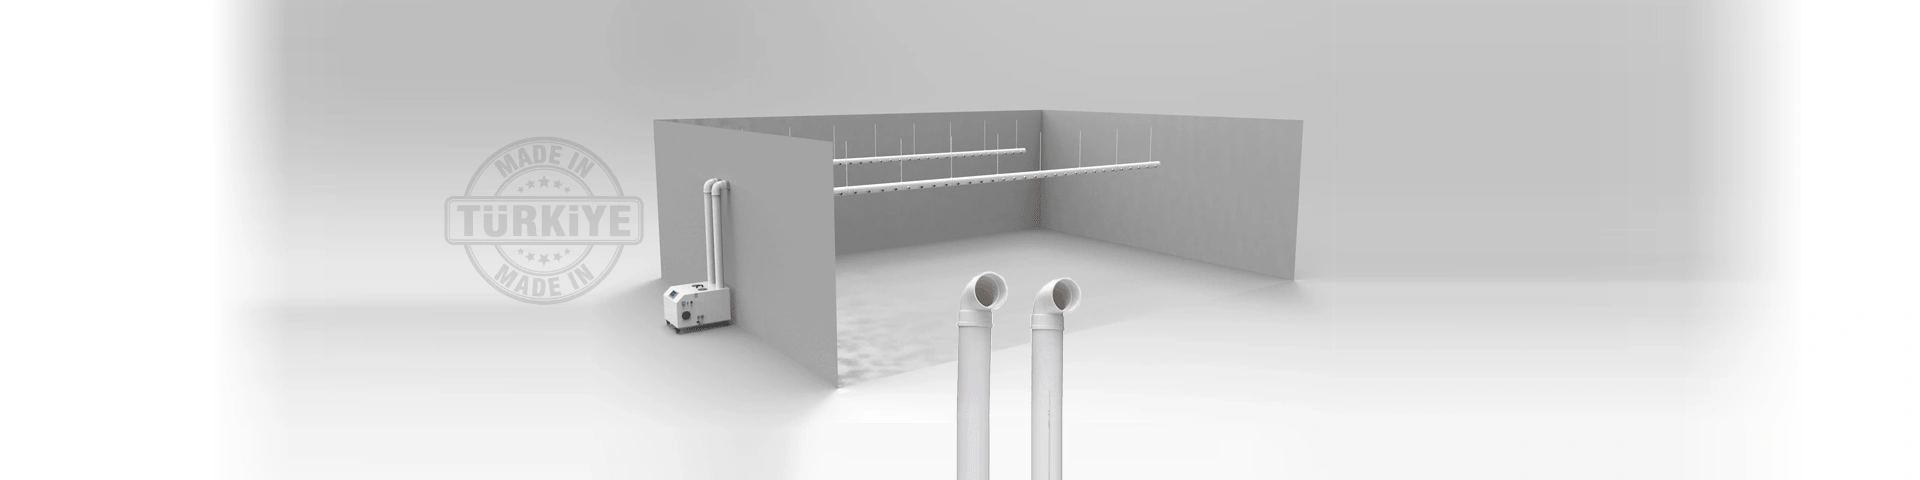
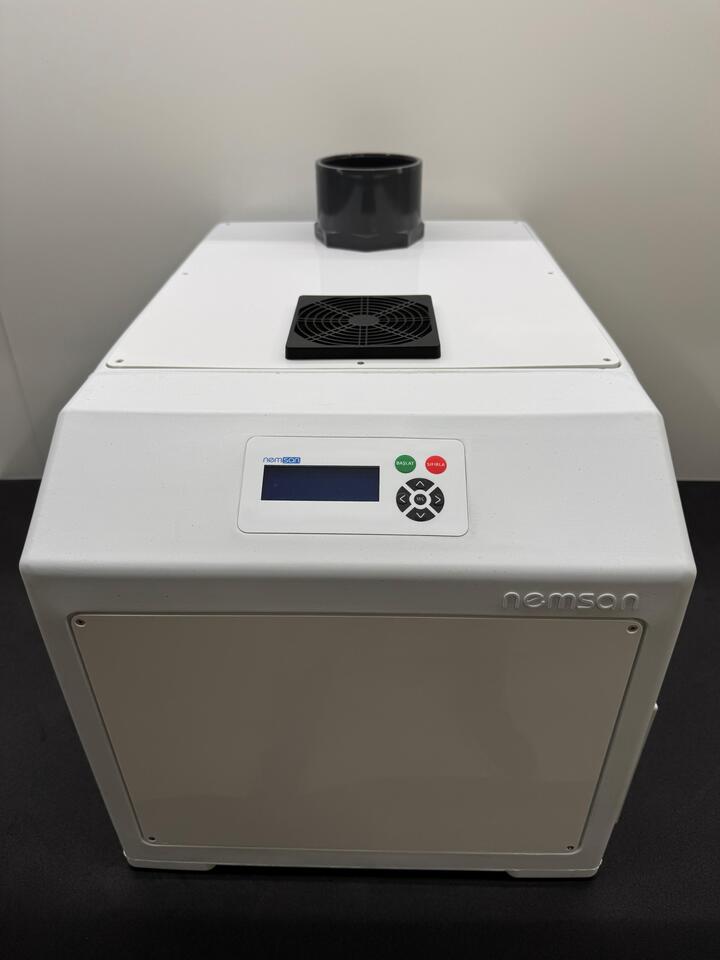
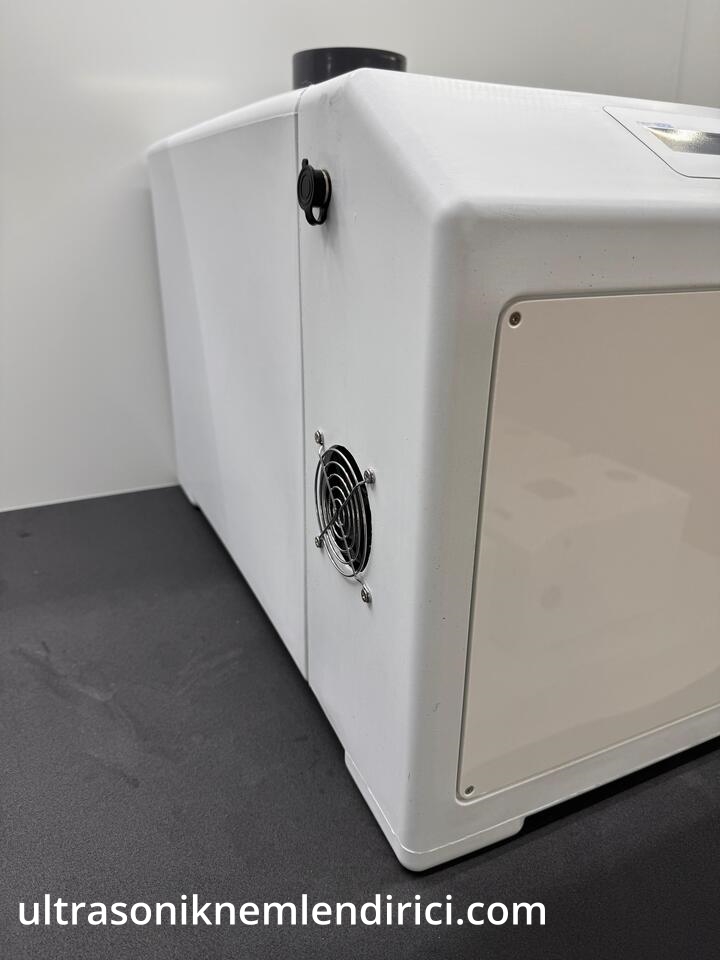
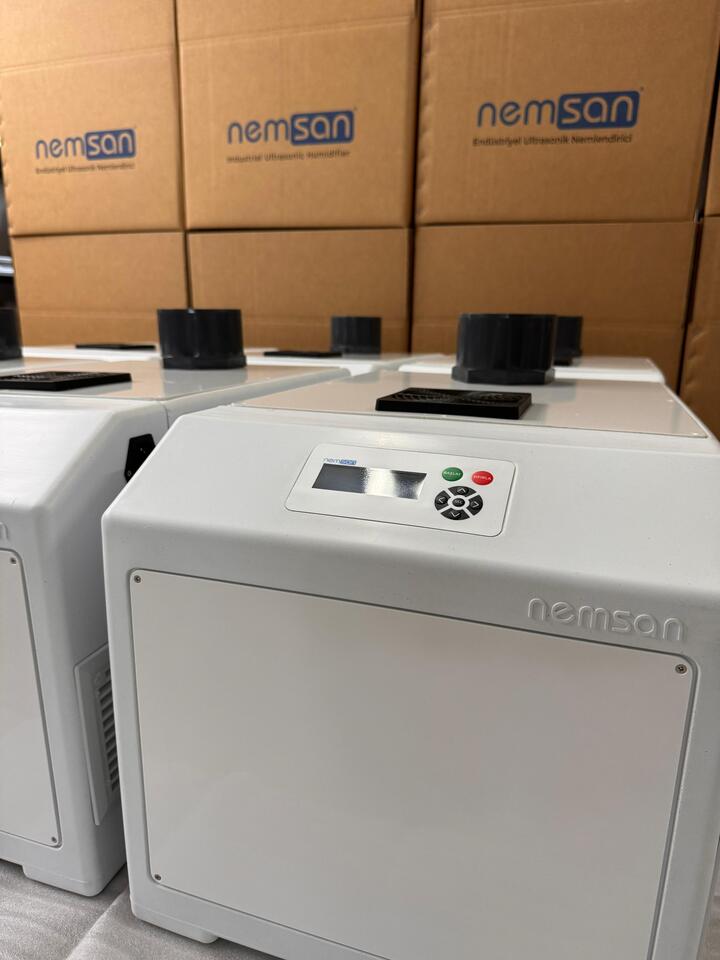
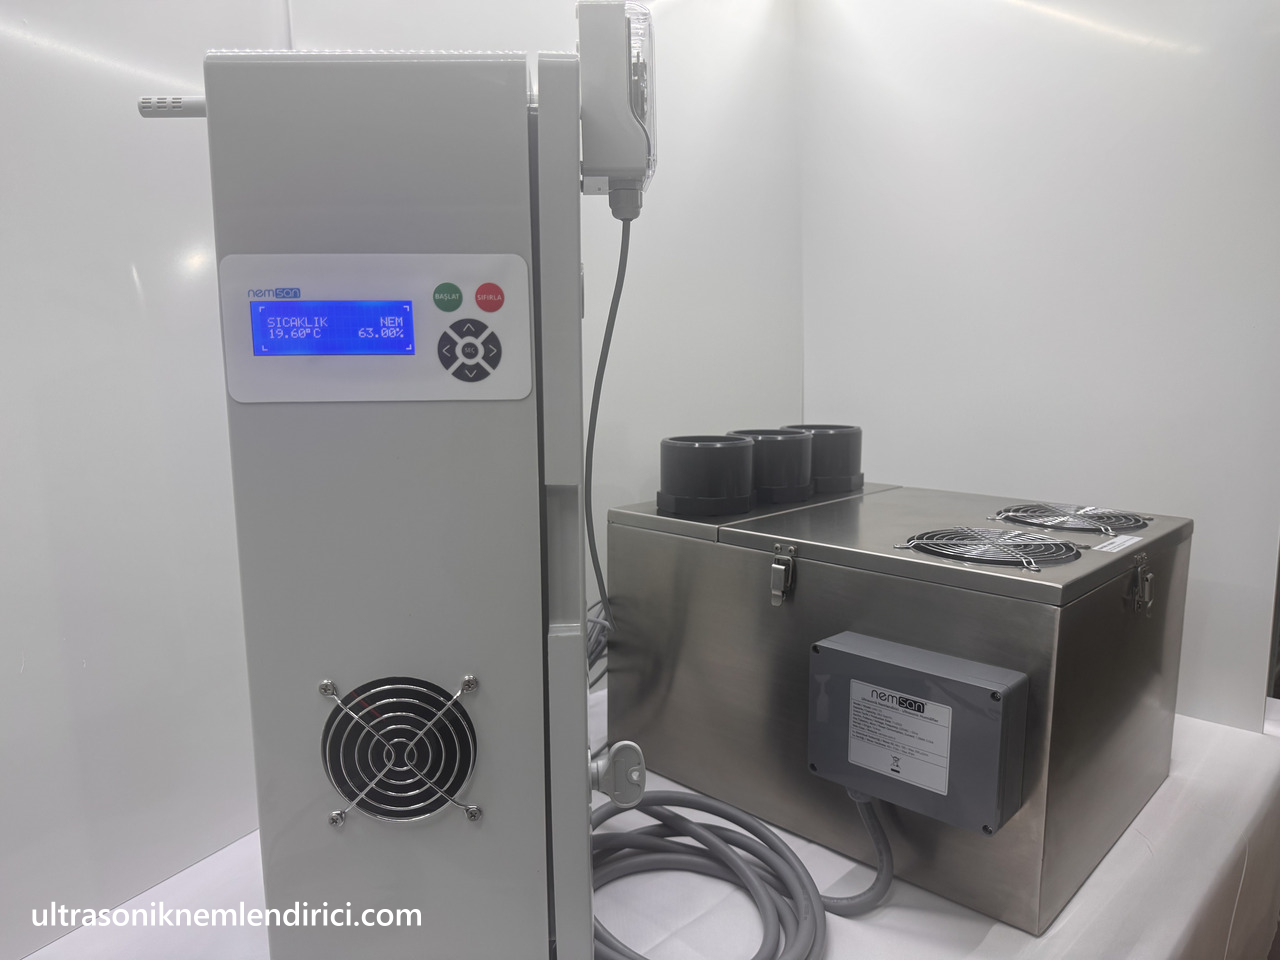
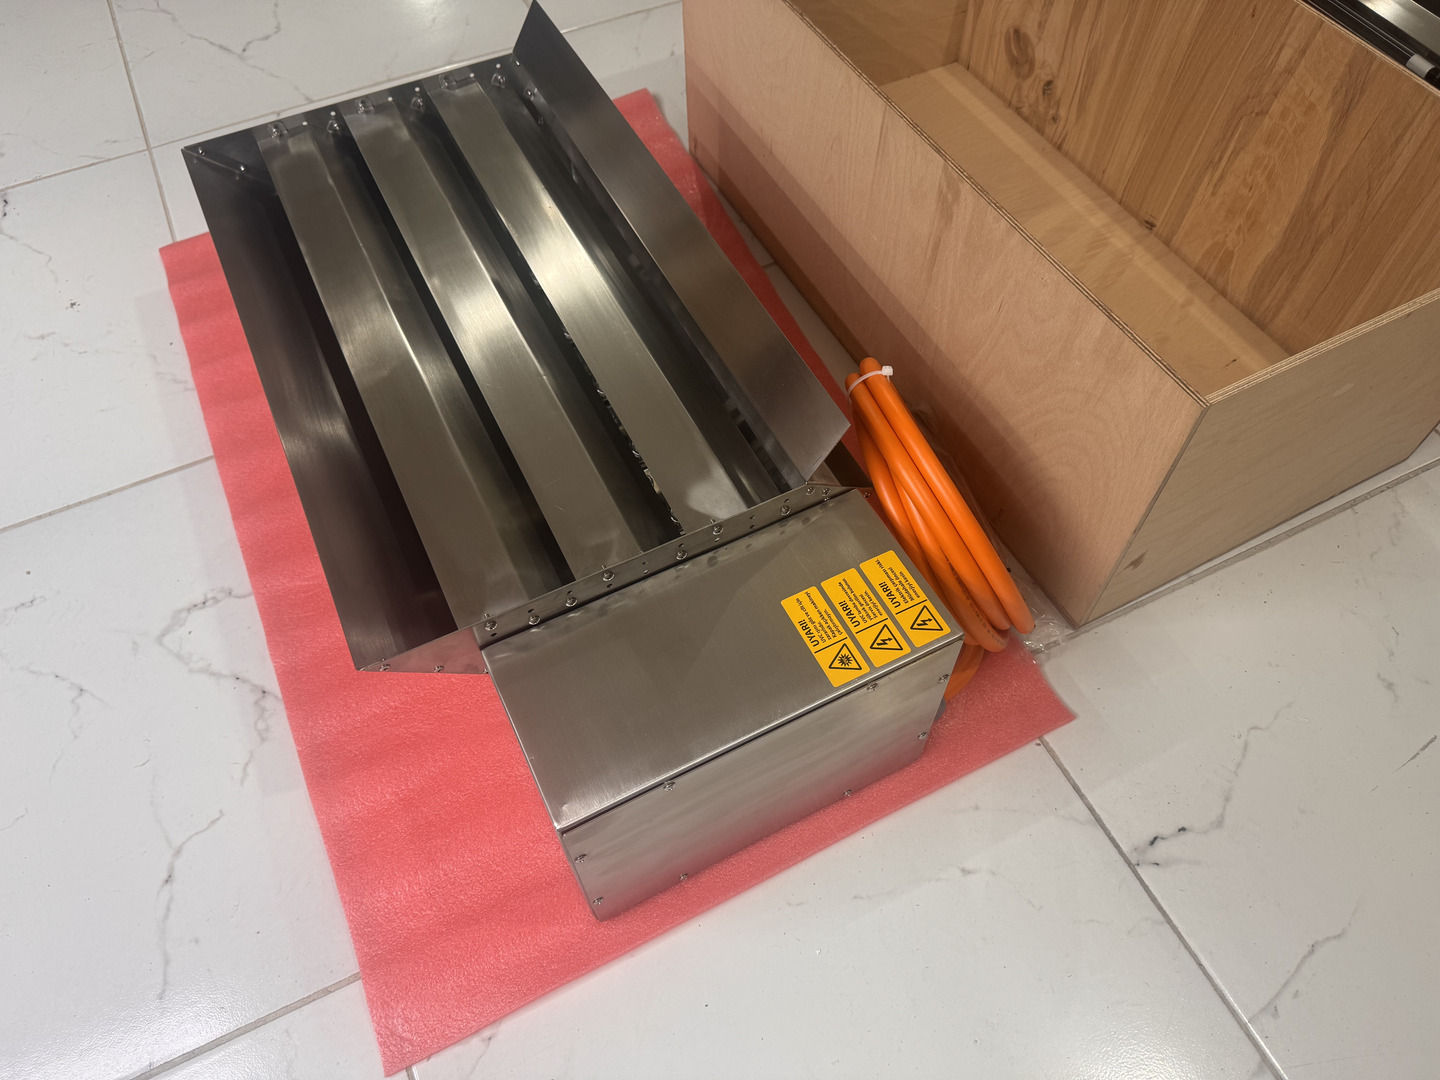
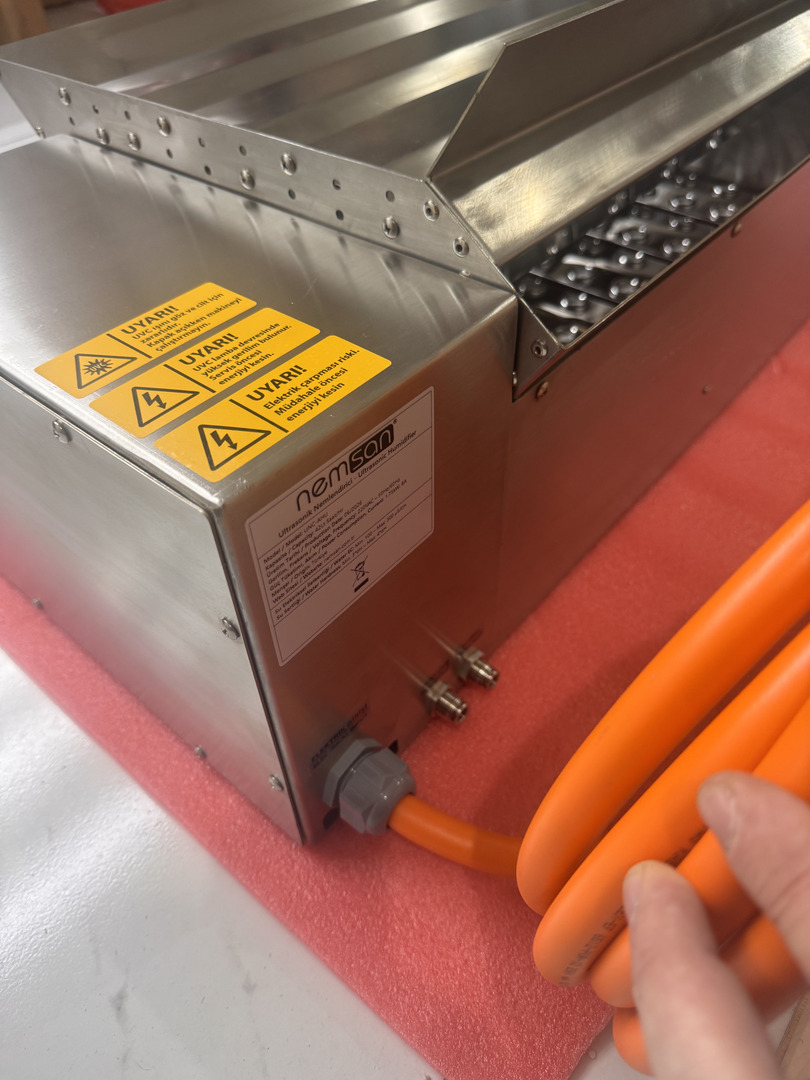
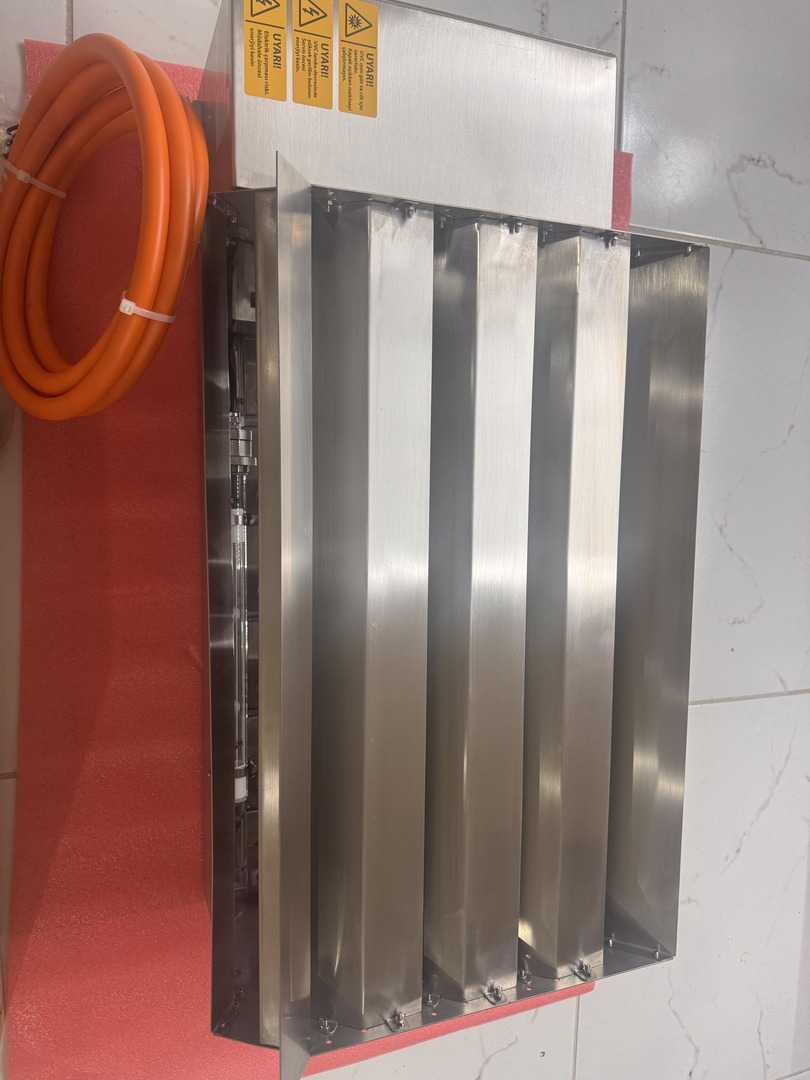
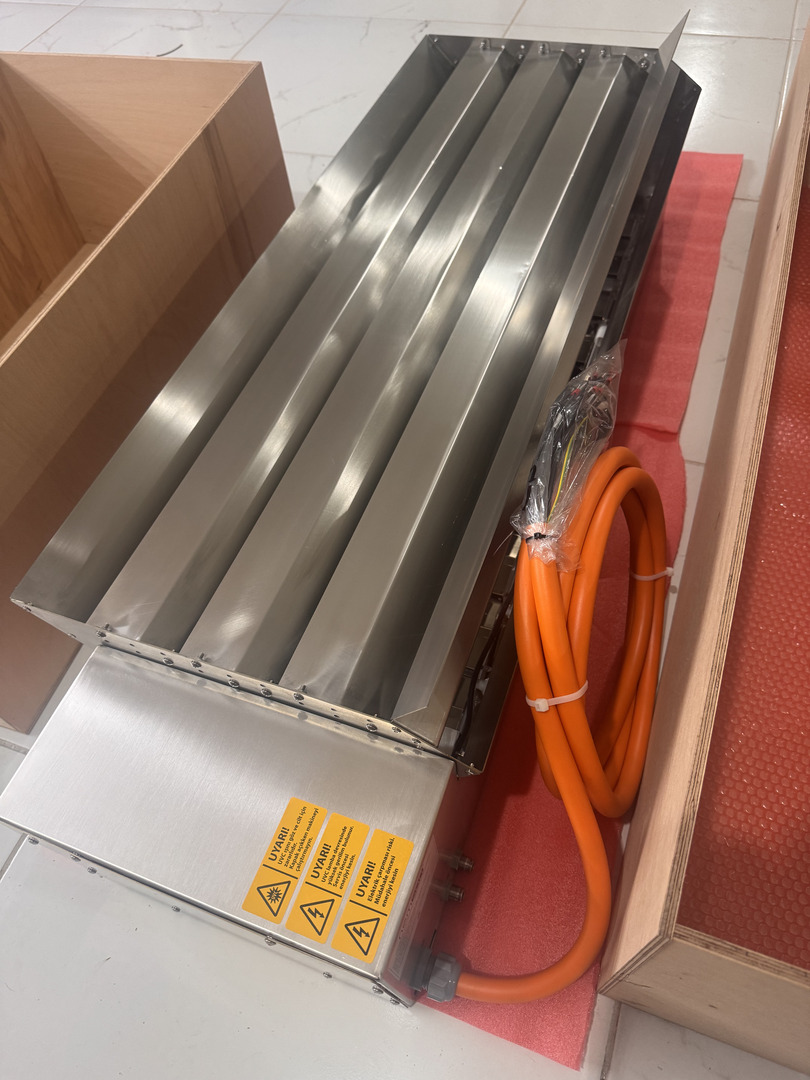
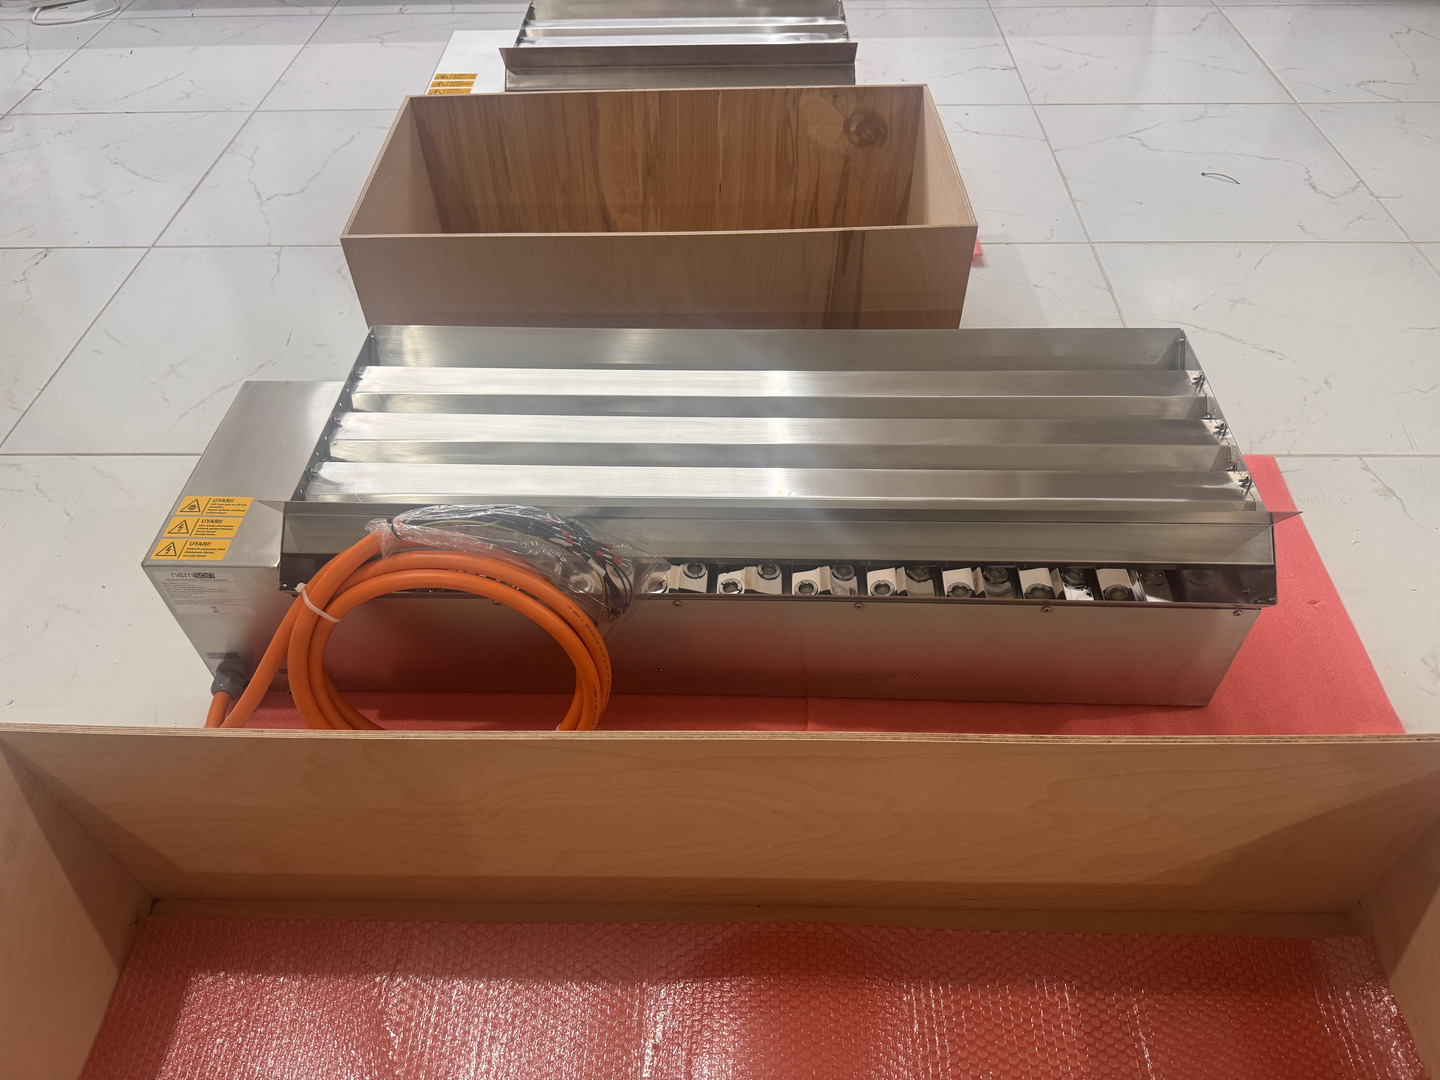
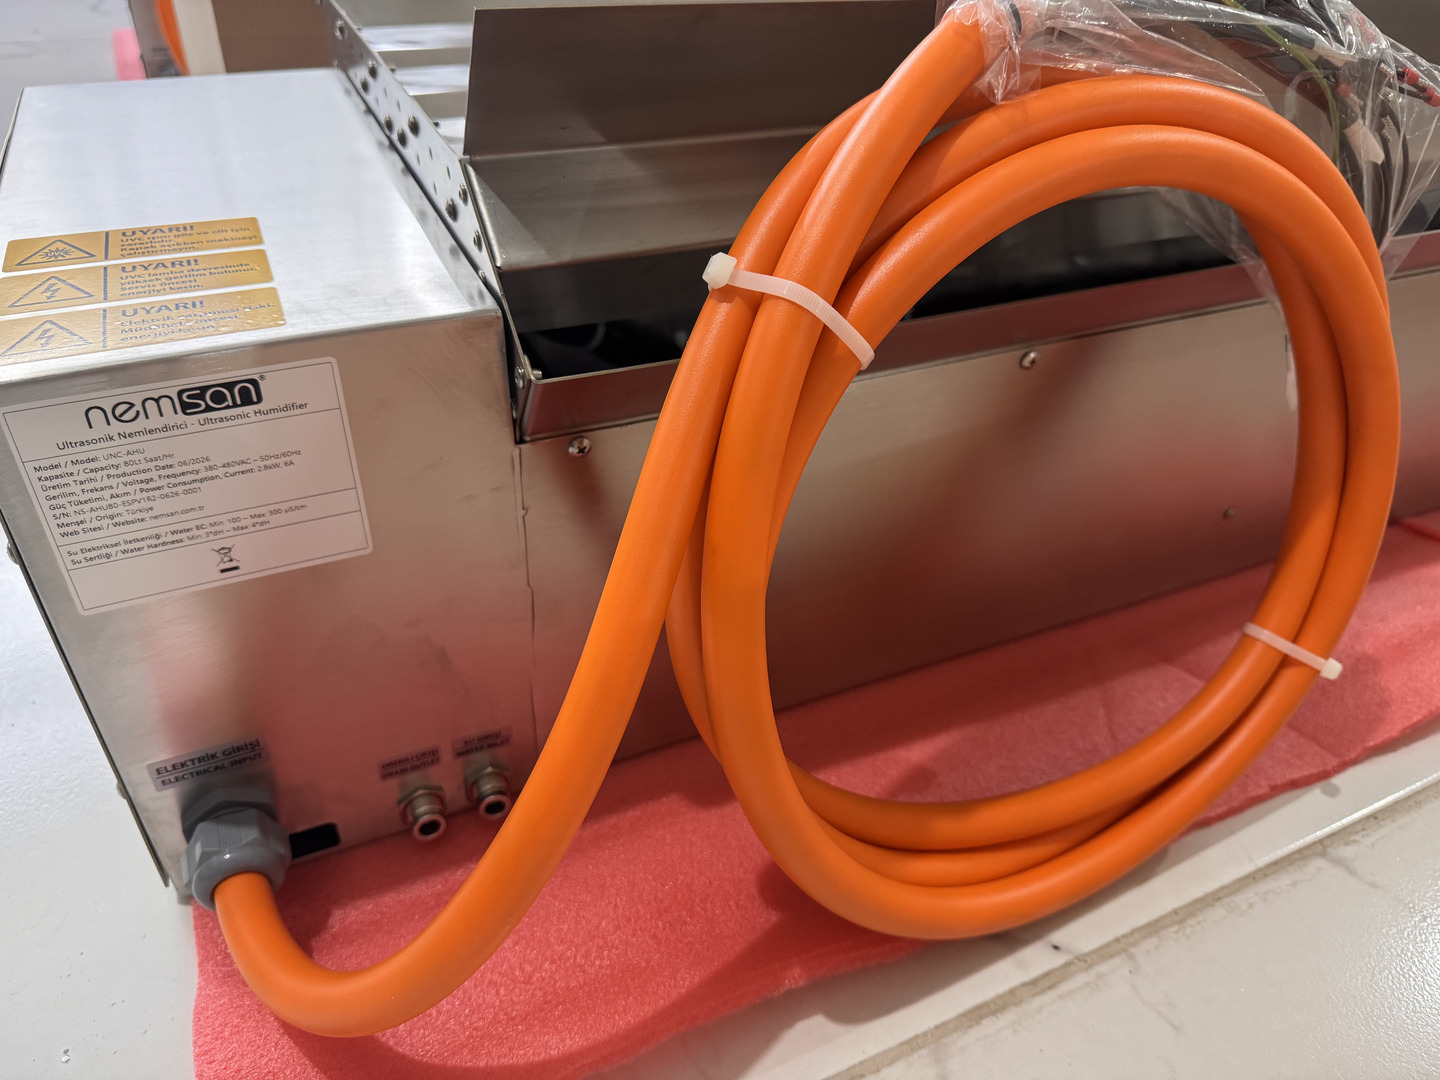
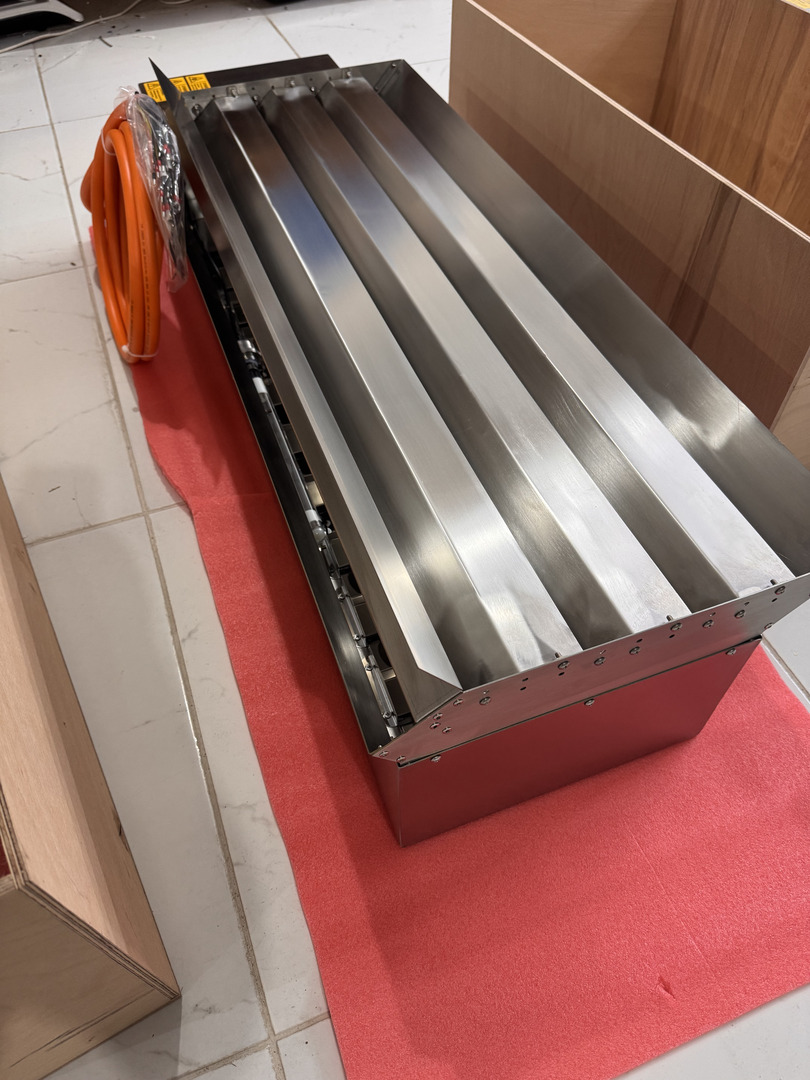
It is a technology that breaks down water with ultrasonic sound waves and converts it from a liquid into cold mist. With piezo motors vibrating at frequencies the human ear cannot hear (Ultra Sound), water of drinking quality is converted into cold mist. It is spread into the environment by means of fans that are not affected by humidity.
Ultrasonic humidifiers are used in many business lines such as cold storages, vegetable/fruit storages, industrial product storage and preservation, bonded warehouses, the warehouses of international cargo companies, poultry farms, worm breeding tents, sheep/cattle barns, vegetable/fruit greenhouses, mushroom production facilities and mushroom farms.
It consumes much less water than conventional pressurised humidification devices. While normal pressurised humidifiers work almost as noisily as a generator, an environment with an ultrasonic humidifier is quiet enough to sleep in. It definitely does not accumulate water on the floor or in the environment. Decay, foaming and deformation due to water and excessive moisture do not occur in the environment. It ensures that humidity spreads perfectly evenly throughout the environment. In mushroom production it makes a high quality and high weight harvest possible. Cold mist also prevents the ambient temperature from rising and provides a natural coolness, reducing your electricity consumption cost.
Around the world, this technology is generally used as the favourite of mushroom growers. Although it is still very new in our country, ultrasonic humidifier technology is used in China and America, the world’s top mushroom producing countries. The word “miracle” is used for this technology. Because ultrasonic humidifiers can meet the moisture needs of mushrooms perfectly, the yield is high and the loss due to wetness is “0”, which is why they are the first choice of professional facilities and conscious producers. Since mushroom production requires precise humidity control 24/7, humidifying the environment with conventional pressurised motors causes excessive water consumption, creates a high noise environment and starts rotting in the production area because the floor is always wet; most importantly, since it soaks the mushrooms, the damage reaches hundreds of kilos in just a single flush. It has been determined by foreign sources that, by preventing the high humidity caused by excessive irrigation which leads to many diseases in cultivated mushroom production, it reduces Spider Web, Wet Bubble and especially Brown Spot disease — which greatly affects yield — by a factor of 10.
If the goal is sustainable production and high efficiency with minimum consumption and labour, the ultrasonic humidifier is a must for your inventory!
Professional Humidity Control with Industrial and Duct Type Ultrasonic Humidifiers
In industrial environments, the correct humidity level is a critical factor for production quality and efficiency. In facilities running sensitive production in particular, the humidity ratio has to be kept under control just as strictly as the temperature. This is exactly where ultrasonic humidifier technology stands out, with its energy savings and precise control capability.
Ultrasonic systems break water down into micron-sized vapour particles using high-frequency vibrations. The desired relative humidity level is therefore reached in a very short time without changing the ambient temperature. This makes them deliver maximum performance in textile, tobacco processing, mushroom growing, printing and electronics manufacturing facilities.
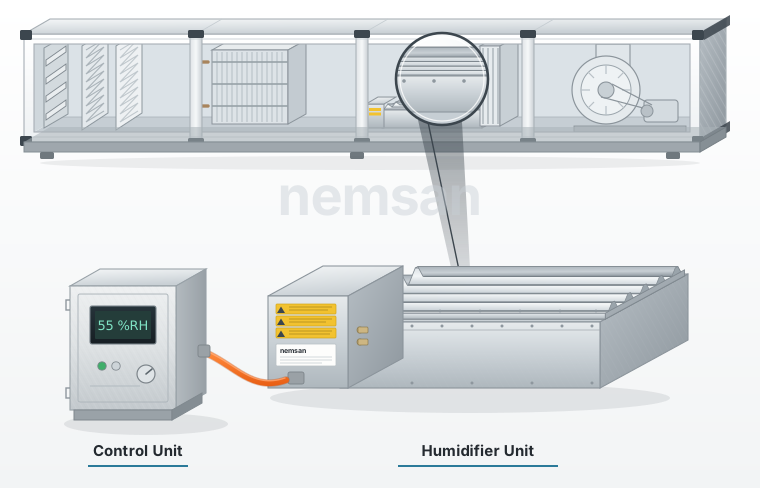
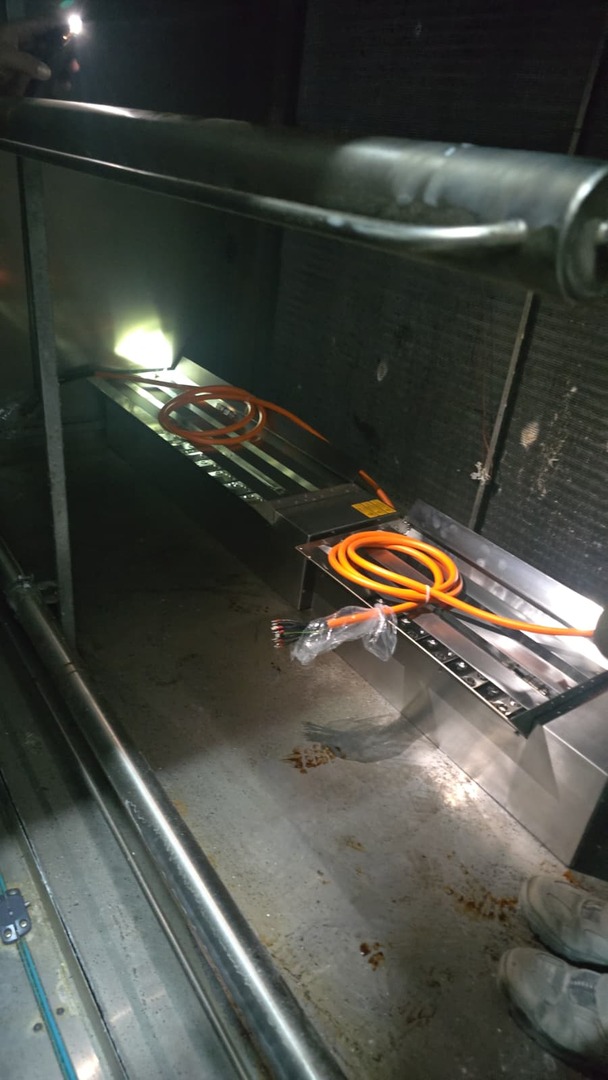
Duct type ultrasonic humidifier models are mounted directly into the air duct and work as an integral part of the air handling system. The cold mist produced in these systems is distributed homogeneously across the whole area through the ducts. As a result, a stable humidity balance is maintained in the environment and production conditions remain consistently steady.
Conventional steam systems consume a great deal of energy because they boil water to create humidity. Ultrasonic humidifiers, on the other hand, evaporate water without heating it, cutting energy consumption by approximately 70–80%. This low energy use offers an environmentally friendly solution and significantly reduces operating expenses.
These systems are also preferred for their ease of maintenance. When used with reverse osmosis or purified water, limescale build-up is kept to a minimum. Regular filter cleaning alone is enough for a long service life. Thanks to their silent operation they can comfortably be used in laboratories, warehouses or offices as well.
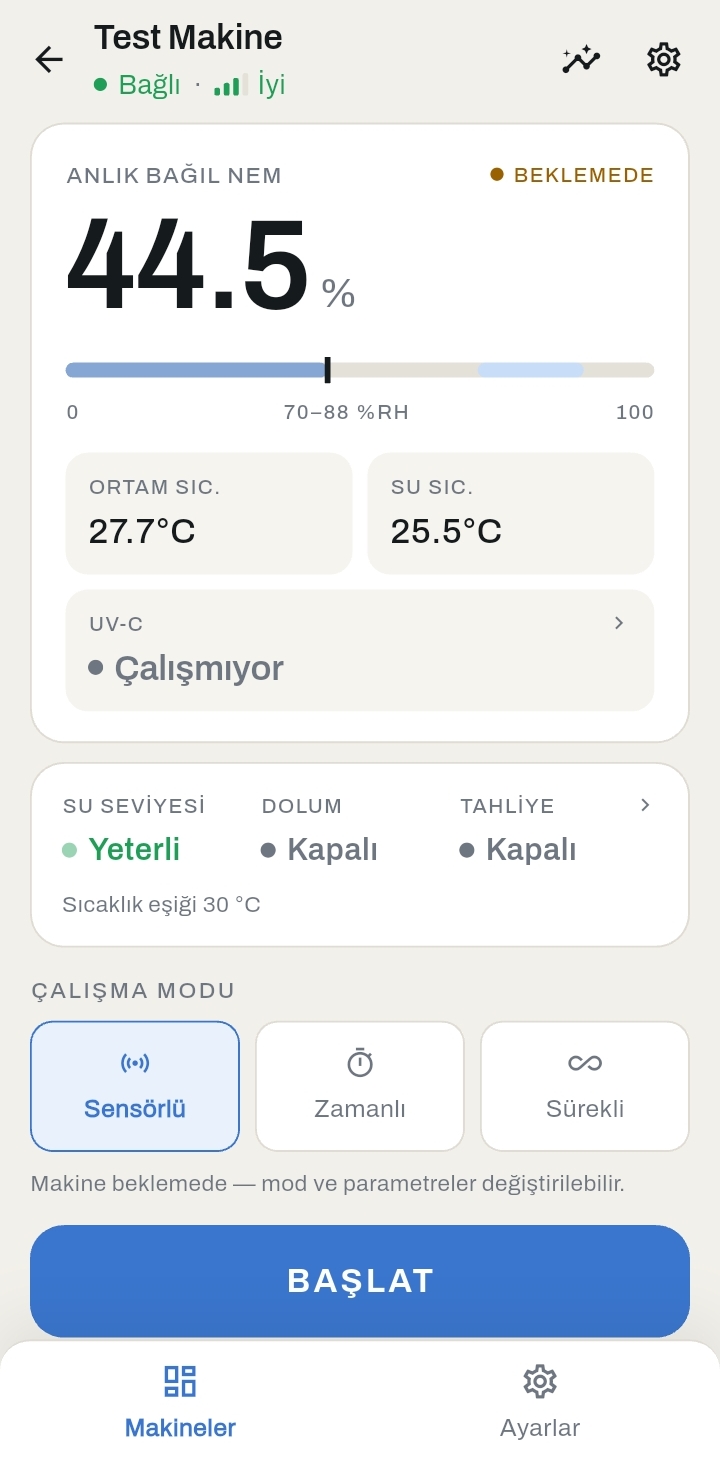
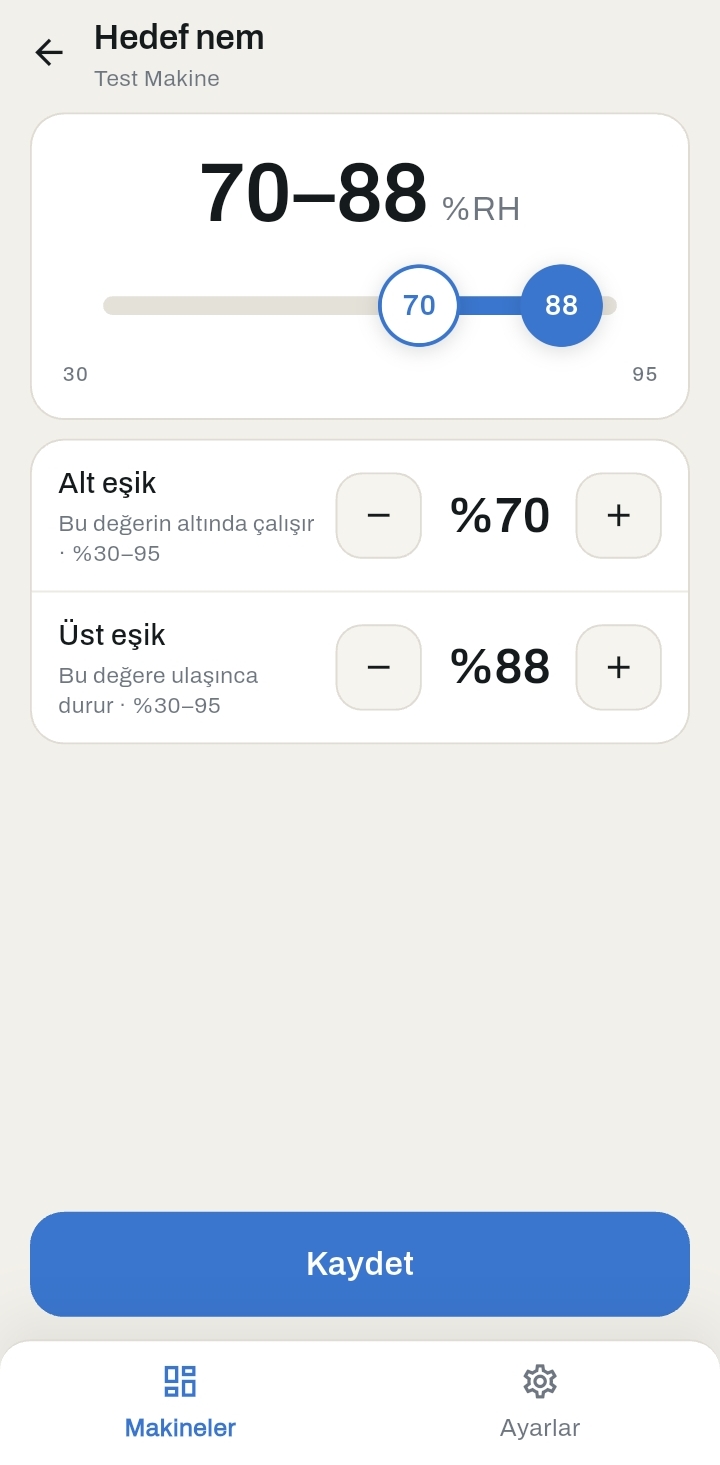
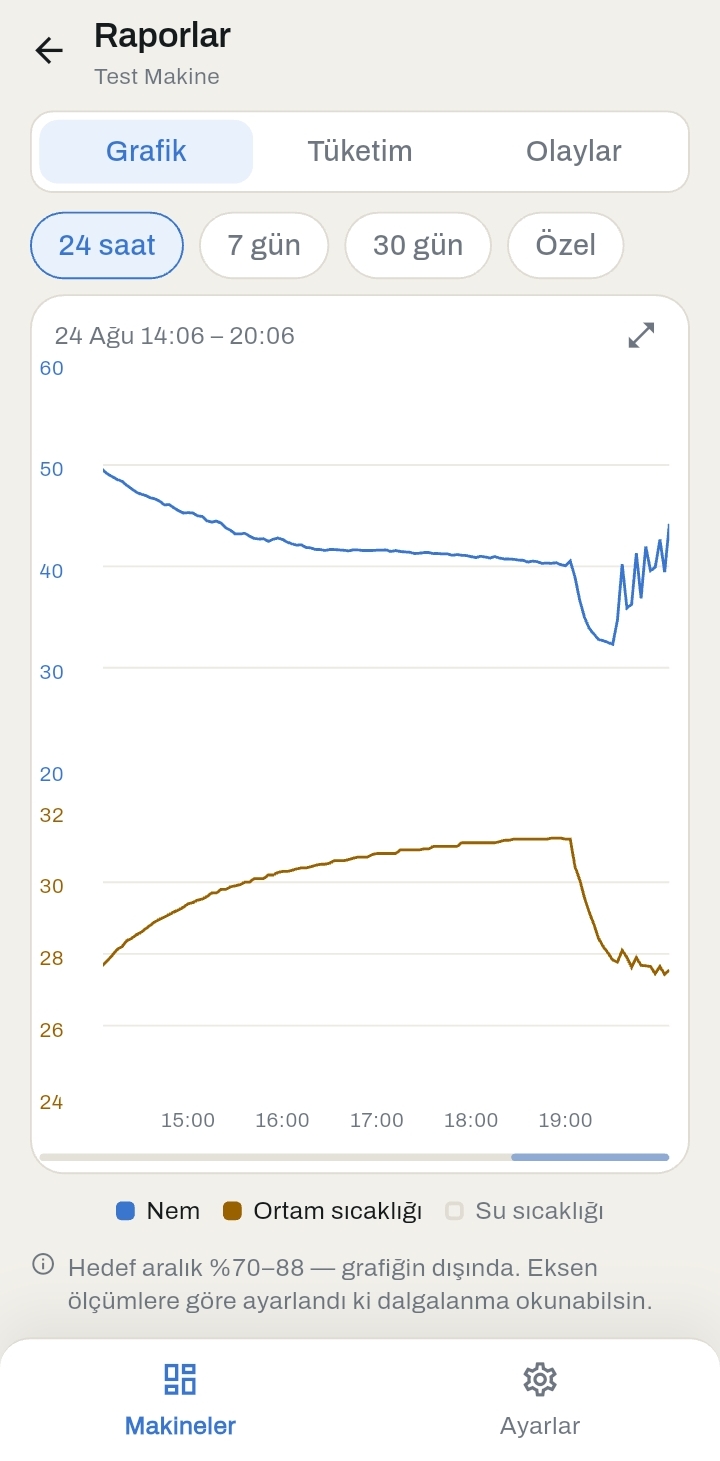
Modern ultrasonic humidifiers are equipped with sensor-based control systems. This allows the unit to start and stop automatically according to ambient humidity. Advanced models also support BMS or Modbus integration, so humidity control can be managed from a central system.
In Türkiye, the Nemsan brand is one of the manufacturers that has adapted this technology to industrial applications most efficiently. The company develops products tailored to the needs of different sectors with its high-capacity industrial and duct type ultrasonic humidifier solutions.
In conclusion, the ultrasonic humidifier is an indispensable component of modern industrial facilities. With advantages such as energy efficiency, silent operation, long service life and low maintenance cost, it both increases production quality and reduces operating expenses. If you want to manage the humidity balance in your facility professionally, this technology is the right solution.